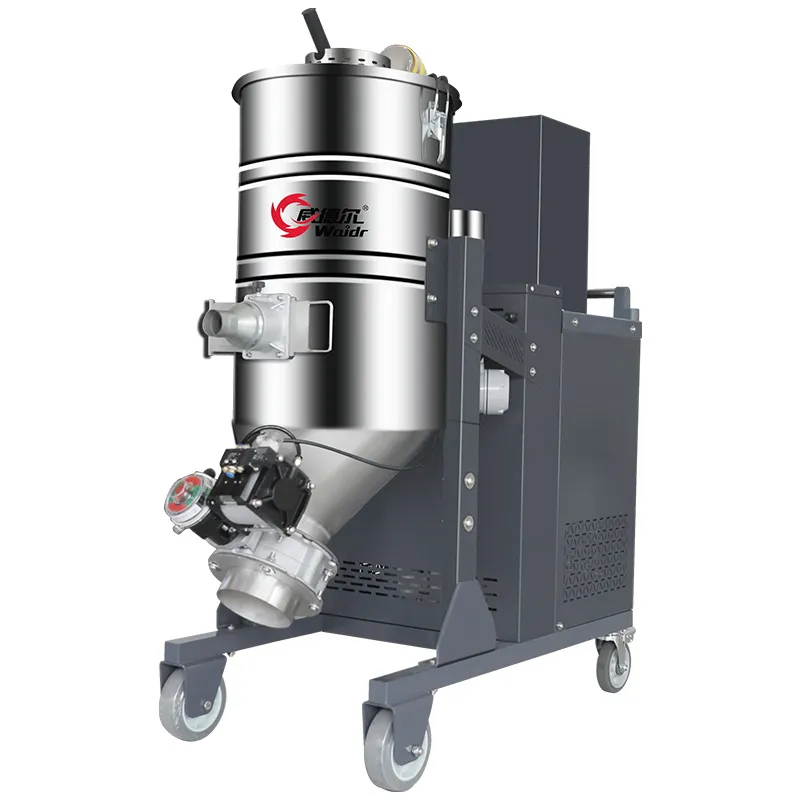

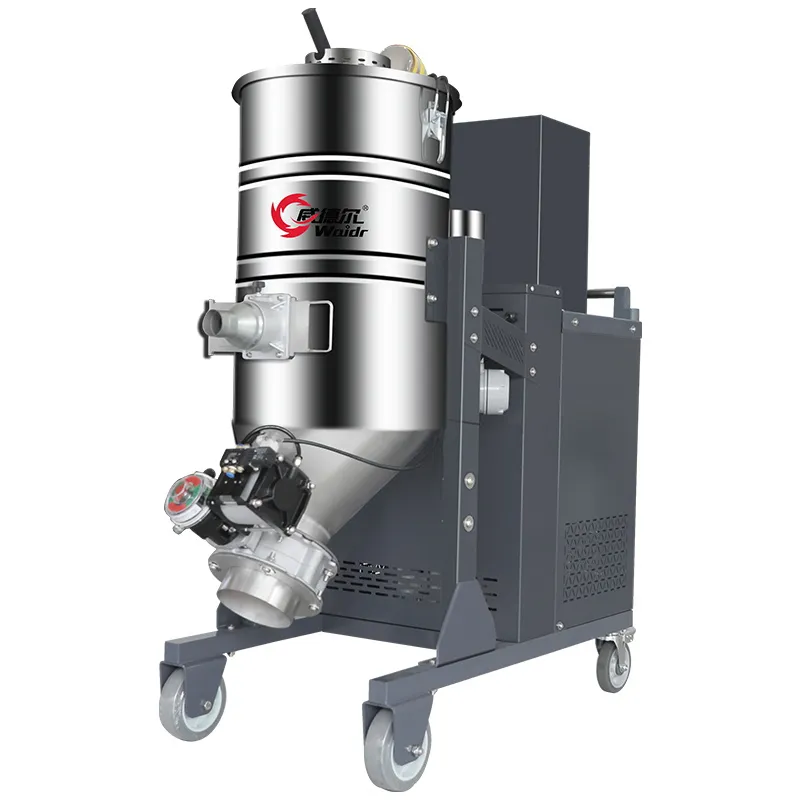
Our industrial vacuum conveyors, serving as a premier vacuum conveyor for industrial application, automate the transfer of powders, granules, and bulk materials with strong suction (200–350 mbar) and high airflow (up to 600 m³/h). Ideal for food, pharmaceutical, and chemical industries, these systems ensure dust-free, hygienic transport with minimal residue, fulfilling the core requirements of a reliable vacuum conveyor for industrial application.
As an industrial vacuum machine supplier, we will do our best to meet all the needs of customers.




















Sign in to leave a comment.