
When a dialysis treatment session begins, most attention naturally goes to the patient, the clinical team, and the dialysis machine. However, behind every successful treatment is a complex supply network that must work with precision. Dialysis machines, water systems, trained professionals, and medical consumables all depend on reliable infrastructure. Among these essential components are haemodialysis concentrates, which are required to prepare the dialysis fluid used during treatment.
A useful example of this changing healthcare focus can be seen at East Kent Hospitals University NHS Foundation Trust, where renal teams reviewed their haemodialysis concentrate supply approach to improve efficiency and reduce environmental impact. The project looked at how concentrates were delivered, stored, and managed rather than changing the clinical treatment itself.
This type of improvement reflects a wider trend across healthcare. Hospitals and renal service providers are increasingly examining the systems behind patient care, including supply reliability, sustainability, and operational efficiency.
For healthcare investors considering a haemodialysis concentrate manufacturing plant in the UK, the opportunity is not simply about setting up a production facility. It requires understanding how healthcare supply chains operate, what quality expectations exist, and what challenges come with manufacturing products used in critical treatments.
A successful facility must combine manufacturing expertise with healthcare discipline. The focus has to be consistent production, controlled processes, and long-term reliability.
The UK Dialysis Market Creates Long-Term Demand for Essential Supplies
Before investing in healthcare manufacturing, understanding demand is essential. Haemodialysis concentrate production is connected directly with the ongoing requirement for kidney replacement therapy.
According to NHS England, approximately 5,500 people start kidney failure treatment every year in England, while around 43,000 people are currently receiving kidney failure treatment. Around 4 in 10 people receiving kidney failure treatment are treated with haemodialysis, where a machine removes waste products and excess fluid from the blood.
These figures matter because haemodialysis is not a short-term healthcare service. Many patients require regular treatment sessions every week, creating continuous demand for the products and systems that support dialysis delivery.
The need for renal services is influenced by several wider health factors, including population ageing, diabetes prevalence, cardiovascular disease, and hypertension. As these conditions continue to affect healthcare demand, renal infrastructure remains an important area of planning.
The UK Kidney Association’s UK Renal Registry monitors kidney replacement therapy activity across renal centres in the UK. This data helps healthcare organisations understand treatment trends and plan future renal services.
For investors, the important point is that dialysis-related manufacturing is linked with a long-term clinical requirement rather than a temporary market opportunity.
Understanding What a Haemodialysis Concentrate Manufacturing Plant Produces
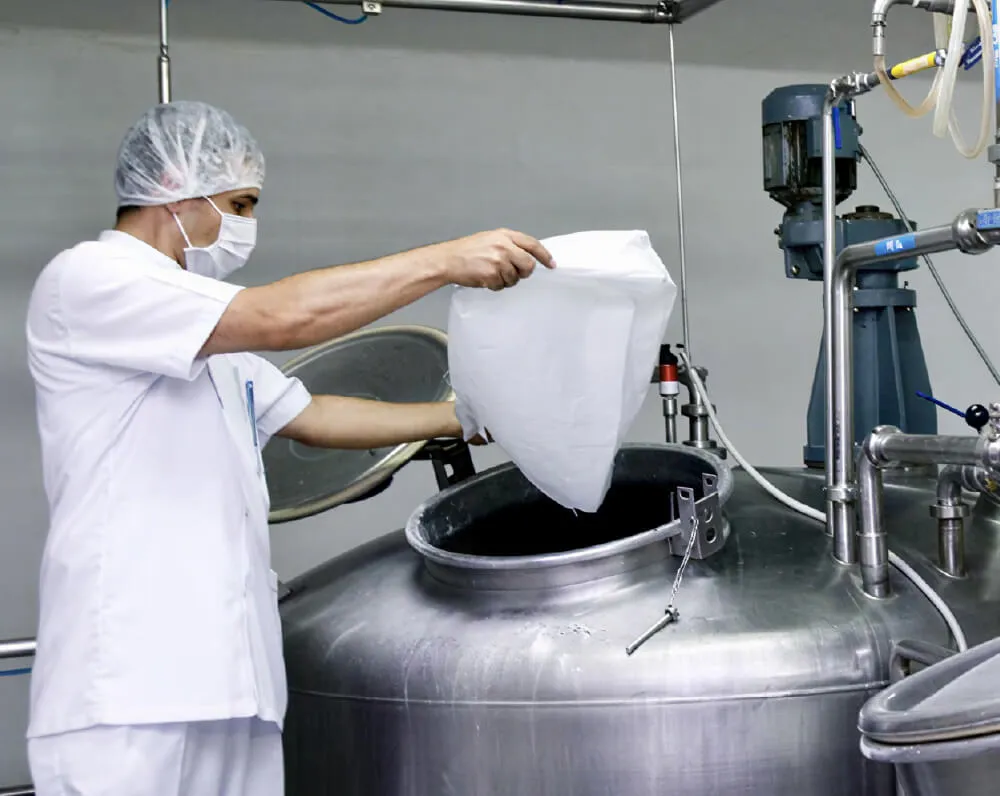
A haemodialysis concentrate manufacturing plant produces specialised concentrated solutions or powders that are later combined with purified water to create dialysis fluid.
During haemodialysis, the patient’s blood passes through a dialysis machine. The machine removes waste products and excess fluid while helping maintain the body’s chemical balance. Dialysis fluid supports this process by creating the correct environment for removing unwanted substances.
The two main concentrate categories used in haemodialysis are:
- Acid concentrate
- Bicarbonate concentrate
These concentrates contain carefully measured chemical components, including electrolytes that are necessary for maintaining the correct balance during treatment.
From a manufacturing perspective, the challenge is precision. The final product must meet strict specifications every time it is produced.
A professional manufacturing operation must control:
- Raw material selection
- Ingredient measurement
- Mixing accuracy
- Product testing
- Packaging quality
- Batch traceability
A mistake in formulation, contamination control, or documentation can create serious quality concerns. This is why haemodialysis concentrate manufacturing requires healthcare-level production standards.
The International Organization for Standardization (ISO) specifically addresses these requirements through ISO 23500-4:2024, which defines chemical and microbiological requirements for concentrates used in haemodialysis and related therapies. The standard applies to manufacturers producing both liquid and powder concentrates.
Investors evaluating this sector should understand that this is not a conventional chemical manufacturing project. It is a regulated healthcare production environment where quality systems are central to commercial success.
A complete production approach fo haemodialysis concentrate manufacturing requires planning around manufacturing technology, quality control, testing procedures, and operational consistency.
Why Supply Chain Reliability Matters in Renal Care
Healthcare supply chains are becoming a strategic priority, especially for products connected with essential treatments.
Dialysis providers operate on fixed treatment schedules. A delay in receiving important supplies can create additional pressure for healthcare teams. This makes reliable availability a critical factor when selecting manufacturing partners.
For investors, this creates an important question:
Can a manufacturing facility solve a real supply chain challenge?
A well-planned UK manufacturing operation may contribute to supply chain flexibility by creating additional production capability closer to healthcare users. However, local manufacturing should complement existing supply networks rather than assume it will replace all international sources.
Healthcare systems usually benefit from having multiple reliable supply options.
The strongest investment cases are built around solving practical problems, such as:
- improving supply reliability
- reducing unnecessary logistics complexity
- supporting sustainable healthcare operations
- improving access to essential products
A successful manufacturer does not only produce a product. It supports the healthcare system that depends on that product.
Powder-Based Dialysis Concentrates: Manufacturing Opportunities and Challenges
Powder-based concentrates are attracting interest because of their potential logistical advantages.
Liquid concentrates contain a significant amount of water, which increases transportation weight and storage requirements. Powder concentrates can provide an alternative approach by allowing more efficient storage and transportation before preparation.
However, powder manufacturing is technically demanding.
The production environment must control factors such as:
- moisture exposure
- powder consistency
- ingredient distribution
- contamination risks
- packaging protection
A powder manufacturing facility requires more than industrial mixing equipment. It needs controlled processes, accurate measurement systems, laboratory capability, and trained operators.
The goal is not simply producing a powder. The goal is producing a healthcare product that performs consistently when used by dialysis providers.
According to ISO 23500-4:2024, the requirements for haemodialysis concentrates apply to both liquid and powder forms, including considerations related to chemical and microbiological quality.
This makes process control one of the most important investment considerations.
A facility with strong quality systems and reliable production methods will generally create more long-term value than a facility focused only on maximum output.
Real UK Examples Showing the Changing Role of Dialysis Supply Management
The importance of improving dialysis supply systems can already be seen through UK healthcare projects.
At East Kent Hospitals University NHS Foundation Trust, renal teams reviewed haemodialysis concentrate practices to improve efficiency and reduce environmental impact. The project demonstrated that changes in concentrate management could create measurable benefits without changing the clinical care provided to patients.
The project achieved an estimated reduction of 16.22 tonnes of CO₂ equivalent per year, showing that improvements in supply management can contribute to healthcare sustainability goals.
Another example comes from Royal Free London NHS Foundation Trust, where renal teams reviewed concentrate usage and identified opportunities to improve resource efficiency and reduce waste.
These examples highlight an important shift in healthcare procurement. Providers are increasingly looking for solutions that combine product quality with operational improvements.
For future manufacturers, understanding these expectations will be important. Healthcare organisations are not only purchasing products; they are looking for dependable partners who understand the challenges of modern renal care.
Designing a Manufacturing Facility Around Healthcare Requirements
Setting up a haemodialysis concentrate manufacturing plant requires much more planning than selecting production equipment and starting operations. The facility itself must support healthcare-level manufacturing standards from the beginning.
The design of the plant influences product quality, operational efficiency, and long-term reliability. A well-planned facility should allow smooth movement of raw materials, controlled production processes, effective testing, and secure storage of finished products.
Important planning areas include:
- production areas suitable for concentrate manufacturing
- laboratory facilities for quality testing
- controlled storage conditions
- packaging and distribution systems
- documentation and traceability processes
The purpose of these systems is to reduce risks and maintain consistency throughout the product lifecycle.
One of the most common mistakes in healthcare manufacturing projects is focusing mainly on machinery while underestimating the importance of process design. Equipment is only one part of the operation. The combination of technology, quality procedures, skilled employees, and management systems determines whether the facility can consistently produce safe products.
For investors, facility planning should be viewed as a long-term decision. A plant designed only for current requirements may struggle if demand increases or healthcare expectations change in the future.
Regulatory Planning and Quality Management in the UK
Healthcare manufacturing requires a strong understanding of regulatory responsibilities. Products connected with dialysis treatment must meet strict expectations because their quality directly affects patient care.
A haemodialysis concentrate manufacturer needs systems that control every stage of production, from incoming materials to final product release.
A strong quality management approach includes:
- supplier qualification
- raw material testing
- controlled manufacturing procedures
- laboratory analysis
- batch documentation
- product traceability
These systems help manufacturers identify problems early and maintain consistent quality.
The ISO 23500 series provides internationally recognised guidance for dialysis fluid preparation and quality management. These standards are widely referenced within the dialysis industry because they address important areas such as water quality, concentrate requirements, and safe dialysis fluid preparation.
For investors, the key lesson is that regulatory planning should begin before production starts. Quality systems influence facility layout, employee training, equipment choices, and operational procedures.
A manufacturing plant that treats compliance as an afterthought may face unnecessary delays and additional costs.
The Importance of Water Quality Knowledge in Dialysis Manufacturing
Water quality plays a central role in dialysis treatment because concentrates are ultimately mixed with purified water to create the final dialysis fluid.
Although concentrate manufacturers are not responsible for every part of the dialysis process, they must understand how their products interact with the wider treatment system.
The ISO 23500 series highlights the importance of controlling chemical and microbiological risks associated with dialysis water and fluid preparation.
This is why dialysis manufacturing requires a healthcare mindset. The product is not simply a chemical mixture. It becomes part of a treatment process where consistency and safety are essential.
For manufacturers, this means investing in:
- reliable testing methods
- qualified laboratory staff
- controlled production environments
- accurate documentation
Understanding the complete dialysis process allows manufacturers to develop products that better meet the practical needs of healthcare providers.
Sustainability Is Becoming a Key Factor in Healthcare Manufacturing Decisions
Healthcare systems are increasingly considering sustainability alongside safety and performance. The NHS has established carbon reduction goals, and healthcare organisations are examining how supply chains contribute to environmental impact.
Dialysis is an area where sustainability improvements can create measurable results because treatment requires continuous use of supplies, transport, packaging, and energy.
Research published in the Journal of Nephrology in 2024 examined the environmental impact of different acid concentrate delivery methods in haemodialysis. The study analysed a 30-station haemodialysis unit and found that alternative approaches could potentially reduce emissions by approximately 33,841 kg CO₂ equivalent per year.
This research shows that supply chain decisions can influence the environmental footprint of dialysis services.
The example from East Kent Hospitals University NHS Foundation Trust also demonstrates how changes in concentrate management can support sustainability. The project achieved an estimated reduction of 16.22 tonnes of CO₂ equivalent per year through improvements in concentrate handling and delivery.
For manufacturers, sustainability is becoming more than an environmental consideration. It is becoming part of how healthcare providers evaluate suppliers.
Future facilities may need to consider:
- efficient packaging
- reduced transport requirements
- improved storage methods
- lower waste generation
The most competitive manufacturers will likely be those that combine quality performance with responsible production practices.
Workforce Planning: Why Technical Expertise Matters
A manufacturing facility is only as strong as the people operating it.
While modern technology can improve production efficiency, skilled professionals are required to maintain quality and solve operational challenges.
A haemodialysis concentrate plant needs employees with knowledge of:
- chemical processing
- quality assurance
- laboratory testing
- manufacturing documentation
- equipment operation
Training should not be limited to production tasks. Employees must understand why accuracy matters and how their role affects healthcare outcomes.
Experienced technical teams can also improve operations over time by identifying ways to reduce waste, improve processes, and strengthen quality systems.
For investors, workforce planning should be included from the beginning. Hiring and training skilled employees takes time and should not be treated as a final step before production.
Investment Risks That Healthcare Investors Should Consider
Like any specialised healthcare manufacturing project, haemodialysis concentrate production involves challenges that need careful planning.
The first challenge is complexity. Manufacturing a dialysis concentrate requires more than creating a chemical formulation. The product must meet strict quality expectations, maintain consistency, and fit into healthcare supply systems.
The second challenge is regulatory responsibility. Quality systems, documentation, and testing requirements require investment and ongoing management.
The third challenge is supply chain control. Manufacturers need reliable access to high-quality raw materials and dependable logistics systems.
Another important consideration is scalability. A facility should be designed with future demand in mind. Healthcare requirements can change, and businesses that cannot adapt may face limitations.
Investors should evaluate the complete lifecycle of the project, including:
- initial facility development
- production operations
- quality management
- maintenance requirements
- future expansion
The strongest investment decisions consider long-term operational performance rather than focusing only on initial setup costs.
Why Supply Chain Resilience Will Shape Future Dialysis Manufacturing
Recent global events have shown healthcare organisations the importance of dependable supply chains.
For dialysis providers, supply continuity is especially important because treatment schedules are closely linked with patient needs.
A manufacturing facility located closer to healthcare users may provide additional flexibility by reducing reliance on complex international logistics.
However, local production alone does not guarantee success. Healthcare providers still require:
- consistent product quality
- reliable delivery
- technical support
- strong communication
The value of a manufacturing facility comes from its ability to solve real healthcare challenges while maintaining high standards.
This is why successful dialysis manufacturing businesses will need to combine production capability with a deep understanding of healthcare operations.
Future Outlook for Haemodialysis Concentrate Manufacturing in the UK
The future of haemodialysis concentrate manufacturing in the UK will be influenced by three major areas: healthcare demand, manufacturing innovation, and supply chain resilience.
The continued need for kidney replacement therapy means dialysis services will remain an important part of healthcare planning.
The UK Kidney Association’s UK Renal Registry continues to monitor renal replacement therapy trends across the UK, helping healthcare organisations understand patient needs and service requirements.
At the same time, manufacturing expectations are changing. Healthcare providers are becoming more interested in suppliers that can demonstrate:
- reliable production
- strong quality systems
- sustainable practices
- operational efficiency
Technology will continue to improve manufacturing through better monitoring systems, automation, and process control. However, technology alone will not determine success.
The companies that perform best will be those that combine technical capability with a clear understanding of healthcare priorities.
Building the Next Generation of UK Renal Care Supply Infrastructure
A haemodialysis concentrate manufacturing plant should not be viewed only as a production facility. It is part of the wider healthcare infrastructure that supports patients receiving essential renal treatment.
The opportunity for investors lies in building a manufacturing operation that solves real healthcare challenges through reliable supply, consistent quality, and responsible production.
The strongest projects will be those that understand the complete picture: dialysis providers need dependable partners, healthcare systems need resilient supply chains, and patients need confidence that essential treatments remain available.
After hours of research into UK renal services, dialysis supply systems, manufacturing standards, and sustainability projects, one conclusion becomes clear: long-term success in this sector depends on combining manufacturing discipline with healthcare responsibility.
A carefully planned haemodialysis concentrate manufacturing facility can contribute to a stronger renal care supply network across the UK by supporting reliable access to essential dialysis materials.
The future of this sector will not be defined only by production capacity. It will be defined by how effectively manufacturers can support safe, efficient, and dependable healthcare delivery.













Sign in to leave a comment.