

Color shapes how we experience the products around us long before we ever read a label or a spec sheet. A fabric's hue, a plastic component's finish, the vibrancy of a printed package, or the appealing tone of a beverage all of these are the result of carefully engineered color science. In modern manufacturing, color is no longer a cosmetic afterthought. It influences consumer perception, brand identity, product functionality, and even regulatory compliance.
Behind every shade lies a defined technology: dyes, pigments, optical brighteners, and food colors each serve a distinct purpose, working through different chemical mechanisms to achieve the desired visual and functional outcome. Understanding the science behind color helps manufacturers, procurement professionals, and industrial buyers make informed decisions about which colorant suits their process, substrate, and end-use requirements.
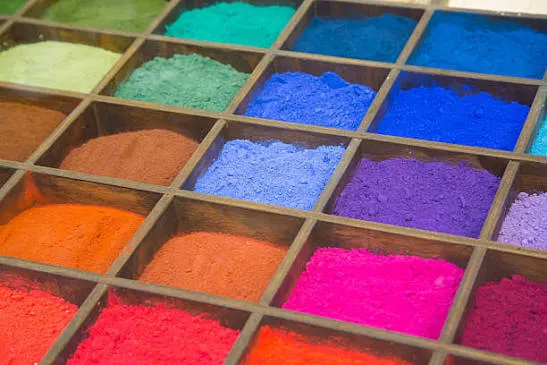
What Is Color Science?
Color, as humans perceive it, is the result of light interacting with a surface. When light strikes an object, certain wavelengths are absorbed while others are reflected back to the eye. The reflected wavelengths are interpreted by the brain as color. A red apple, for instance, absorbs most wavelengths of visible light except those in the red spectrum, which it reflects.
This principle of absorption and reflection is the foundation of industrial color science. Chemists and manufacturers exploit these light-interaction properties by designing molecules - dyes and pigments that absorb specific wavelengths consistently and predictably. The stability of this interaction under heat, light, and chemical exposure determines how well a colorant performs in real-world conditions, whether that's a garment exposed to sunlight or a food product stored on a shelf for months.
Understanding this science is essential for industries that depend on consistent, reproducible color across large production batches
Understanding Dyes
Dyes are colored substances that have a chemical affinity for the material they are applied to, known as the substrate. Unlike surface coatings, dyes actually bond with the substrate at a molecular level, either through absorption, chemical reaction, or ionic attraction. This is why dyed textiles retain color even after repeated washing the dye molecule has become chemically attached to the fiber rather than simply sitting on its surface.
There are several major categories of dyes, including direct dyes, reactive dyes, acid dyes, and basic dyes, each suited to different fiber types and processing conditions. Dyestuffs are widely used across textiles, paper, leather, inks, and various specialty applications where deep, uniform coloration is required.
Benefits of dyes include vibrant color output, transparency, and strong compatibility with natural and synthetic fibers. However, dyes are generally soluble in the application medium, which can make them more susceptible to fading under prolonged UV exposure or repeated washing compared to pigments, depending on the fastness grade selected.
Understanding Pigments
Pigments differ fundamentally from dyes in how they achieve color. Rather than dissolving into the substrate, pigments are insoluble particles that are dispersed throughout a medium paint, plastic, ink, or coating where they remain as discrete solid particles. Color is achieved through the way these particles scatter and reflect light rather than through chemical bonding.
Pigments fall into two broad categories: organic pigments, derived from carbon-based compounds and known for bright, intense shades, and inorganic pigments, typically metal oxide-based and valued for excellent heat stability and opacity. Pigments are essential in paints, coatings, plastics, printing inks, construction materials, and cosmetics, where durability and resistance to environmental degradation are priorities.
The key advantage of pigments lies in their superior lightfastness and chemical resistance, making them the preferred choice for outdoor applications, automotive coatings, and long-life plastic products.
Understanding Optical Brighteners
Optical brighteners, also called fluorescent whitening agents, work differently from both dyes and pigments. Instead of adding color in the traditional sense, they absorb invisible ultraviolet light and re-emit it as visible blue light. This process counteracts the natural yellowish tint found in many raw materials, making fabrics, papers, and plastics appear whiter and brighter than they would otherwise.
Optical brighteners are widely used in textile finishing, laundry detergents, paper manufacturing, and plastic packaging. For manufacturers, they offer a cost-effective way to enhance perceived product quality without altering the base formulation. For end users, the result is a visibly cleaner, crisper appearance in everyday products — from white bedsheets to printer paper.
Understanding Food Colors
Food colors are additives used to enhance or restore the visual appeal of food and beverage products. They fall into two broad groups: natural food colors, extracted from sources such as beet juice, turmeric, or annatto, and synthetic food colors, manufactured to precise specifications for stability and consistency.
Food colors play a critical role in consumer acceptance color often signals freshness, flavor, and quality before a product is even tasted. Their applications span bakery items, confectionery, beverages, dairy products, processed foods, and even pharmaceutical formulations, where consistent, regulation-compliant coloration is essential for both branding and safety compliance.
Industrial Importance of Color Technologies
Color technologies underpin production quality and brand consistency across a wide range of sectors.
In the textile industry, dyes determine fabric vibrancy and washfastness, while optical brighteners enhance whiteness in finished garments. The paint and coating industry relies heavily on pigments for opacity, weather resistance, and long-term color retention on exposed surfaces. In the plastic industry, pigments must withstand high processing temperatures without degrading, while maintaining uniform dispersion throughout the polymer matrix.
The printing ink industry depends on both dyes and pigments depending on the substrate and desired finish, while the paper industry uses optical brighteners extensively to achieve the crisp white tone associated with premium paper products. In the food and beverage industry, food colors are indispensable for product appeal and brand recognition, and the pharmaceutical industry uses both food-grade colors and specialty dyes for tablet coating, capsule identification, and formulation branding.
How Manufacturers Choose the Right Color Solution
Selecting the appropriate colorant involves balancing several technical and commercial factors:
- End-use application - the substrate and processing method largely dictate whether a dye or pigment is suitable.
- Regulatory requirements - particularly critical for food, pharmaceutical, and cosmetic applications, where compliance with safety standards is non-negotiable.
- Color consistency - batch-to-batch uniformity is essential for brands maintaining a recognizable identity.
- Heat resistance - relevant for plastics and coatings processed at high temperatures.
- Light fastness - determines how well a color withstands prolonged sun or UV exposure without fading.
- Chemical resistance - important for products exposed to solvents, detergents, or industrial cleaning agents.
- Cost-effectiveness - balancing performance requirements against production budgets and order volumes.
Manufacturers who evaluate these factors carefully are better positioned to avoid costly reformulations and ensure their products meet both aesthetic and functional expectations.
The Role of Megha International
Meeting these varied technical requirements calls for a supplier with broad formulation expertise and consistent quality control. Megha International has built its reputation as a manufacturer and exporter offering a comprehensive range of dyestuffs, pigments, optical brighteners, and food colors, catering to industries ranging from textiles and plastics to food processing and pharmaceuticals.
By maintaining strict quality standards across its production chain, Megha International supports manufacturers in achieving reliable, application-specific color solutions whether the requirement is a colorfast reactive dye for textile processing, a heat-stable pigment for plastic molding, or a food-grade colorant compliant with industry regulations. This breadth of offering allows buyers to source multiple color technologies from a single, quality-focused partner rather than managing several vendor relationships.
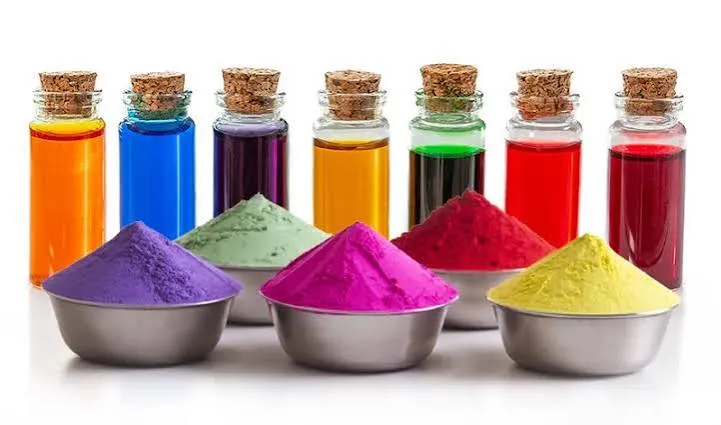
Conclusion
The science behind color is far more intricate than it appears on the surface. Dyes, pigments, optical brighteners, and food colors each rely on distinct chemical and physical mechanisms to achieve their effects, and each is suited to specific substrates, industries, and performance requirements. For manufacturers, understanding these differences is the first step toward selecting colorants that deliver consistent, durable, and compliant results.
As industries continue to demand higher performance and stricter regulatory compliance, the value of working with experienced, quality-driven color solution providers becomes increasingly clear. Whether the application involves textiles, plastics, paints, or food products, choosing the right color technology backed by reliable manufacturing expertise remains central to product success.














Sign in to leave a comment.