

Introduction
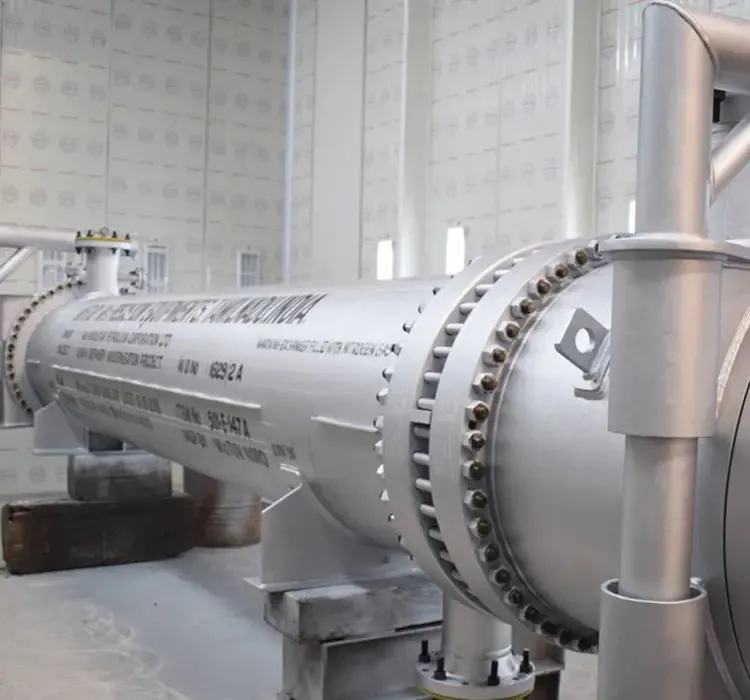
Non Ferrous Heat Exchanger Manufacturer is often one of the first search terms used by procurement teams and plant engineers when sourcing reliable thermal equipment. In industries such as Oil & Gas, Petrochemicals, Fertilizers, Chemicals, LNG, FSRU, FPSO, Renewable Energy and Data Centre Cooling, selecting the right manufacturing partner is about far more than price. It is a decision that directly affects plant efficiency, safety, operational continuity and long term sustainability.
Heat exchangers operate under demanding conditions where high pressures, corrosive fluids and extreme temperatures are part of daily operations. Equipment failure can lead to costly shutdowns, reduced productivity and increased maintenance expenses. This is why choosing an experienced Non Ferrous Heat Exchanger Manufacturer requires careful evaluation based on engineering expertise, manufacturing quality and proven industry experience.
Whether planning a new facility or upgrading existing equipment, understanding what separates an exceptional manufacturer from an average supplier helps organisations make informed decisions that deliver lasting value.
Why Manufacturer Selection Matters
Critical process industries rely on continuous production. Every component must perform consistently, even in the harshest operating environments.
Heat exchangers manufactured from non ferrous materials such as copper nickel, titanium, aluminium bronze and other specialised alloys provide excellent corrosion resistance, longer service life and improved thermal performance. However, these benefits can only be achieved when the equipment is designed and manufactured to the highest standards.
An experienced Non Ferrous Heat Exchanger Manufacturer understands material behaviour, fabrication techniques and application specific engineering requirements, ensuring every unit meets operational expectations.
Evaluate Industry Experience
Experience is often the strongest indicator of long term reliability.
Manufacturers serving sectors such as Oil & Gas, Petrochemicals and LNG understand the operational challenges associated with corrosive media, fluctuating temperatures and demanding pressure conditions. Their knowledge enables them to recommend suitable materials, optimise thermal performance and minimise operational risks.
Look for manufacturers with successful project experience across multiple industries rather than those offering generic solutions.
Assess Engineering and Design Capabilities
Every industrial process has unique thermal requirements.
A capable manufacturer should provide customised engineering rather than relying solely on standard catalogue products. Design expertise should include thermal calculations, mechanical design, material compatibility analysis and optimisation for plant specific conditions.
An experienced Non Ferrous Heat Exchanger Manufacturer will work closely with customers to develop equipment that balances performance, durability and maintenance requirements throughout its lifecycle.
Verify Material Expertise
Material selection has a significant influence on heat exchanger performance.
Different process environments demand different alloys. For example, seawater cooling systems often require copper nickel or titanium, while chemical processing may require specialised corrosion resistant materials.
Manufacturers should demonstrate extensive knowledge of:
- Corrosion resistance
- Thermal conductivity
- Mechanical strength
- Fabrication methods
- Long term material reliability
This expertise helps ensure the equipment performs efficiently throughout its intended service life.
Review Manufacturing Standards and Certifications
Manufacturing quality should never be overlooked.
Reputable manufacturers operate according to internationally recognised quality management systems and industry standards. Certifications demonstrate a commitment to consistent production quality and regulatory compliance.
Important considerations include:
- ASME manufacturing capabilities
- ISO quality management certification
- Qualified welding procedures
- Certified inspection personnel
- Material traceability systems
These standards contribute directly to equipment reliability and customer confidence.
Key Questions to Ask Before Choosing a Manufacturer
Before making a purchasing decision, consider asking the following questions:
- Do they manufacture customised solutions?
Custom designs usually deliver better performance than standard equipment. - Can they support specialised non ferrous materials?
Material expertise is essential for demanding industrial applications. - What testing procedures are performed?
Hydrostatic, pneumatic and non destructive testing improve reliability. - Do they provide engineering support?
Technical guidance helps optimise equipment selection. - What industries do they regularly serve?
Relevant project experience reduces implementation risks. - Is after sales support available?
Reliable technical assistance simplifies maintenance and future upgrades.
Evaluate Manufacturing Infrastructure
Modern manufacturing facilities often produce higher quality equipment with greater consistency.
Advanced fabrication technologies, precision machining, automated welding and comprehensive inspection processes improve dimensional accuracy and product reliability.
Factory capabilities should also include:
- Dedicated fabrication workshops
- CNC machining facilities
- Non destructive examination equipment
- Pressure testing facilities
- Performance testing procedures
A well equipped facility demonstrates commitment to manufacturing excellence.
Focus on Quality Rather Than Initial Cost
Choosing the lowest quotation can become expensive over time.
A high quality heat exchanger generally offers longer operating life, fewer maintenance requirements and greater energy efficiency. Lower maintenance costs and reduced downtime often outweigh the difference in initial purchase price.
Working with a trusted Non Ferrous Heat Exchanger Manufacturer helps reduce lifecycle costs while improving operational reliability.
Consider Sustainability and Energy Efficiency
Sustainability has become an important purchasing consideration across critical industries.
Efficient heat exchangers recover more energy, reduce process losses and support lower carbon emissions. Manufacturers investing in innovative thermal design contribute to improved plant efficiency and environmental performance.
Industrial buyers increasingly evaluate suppliers based on both technical capability and sustainable manufacturing practices.
Look for Long Term Partnership Value
The relationship should not end after equipment delivery.
Reliable manufacturers provide documentation, technical consultation, maintenance recommendations and replacement support throughout the equipment lifecycle.
Long term partnerships often result in improved plant performance because manufacturers gain a deeper understanding of operational requirements over time.
Selecting an experienced Non Ferrous Heat Exchanger Manufacturer means investing in ongoing technical expertise rather than simply purchasing equipment.
Conclusion
Selecting the right heat exchanger manufacturer is a strategic investment that influences operational efficiency, plant safety and long term reliability. Evaluating engineering expertise, manufacturing capabilities, quality systems, material knowledge and industry experience enables organisations to make confident purchasing decisions that support continuous production.
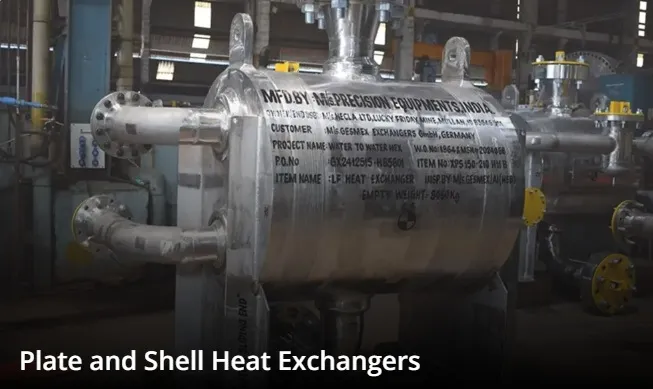
For critical industries, dependable thermal equipment remains essential for achieving operational excellence and sustainable growth. Companies with decades of engineering expertise often provide valuable insight into evolving industry requirements. Precision Equipments has been a leading manufacturer and supplier of Shell and Tube Heat Exchangers and process equipment since 1981, serving key sectors such as Oil & Gas, Petrochemicals, Fertilizers, Power Plants, LNG and Nuclear Energy. This long standing experience reflects the importance of selecting manufacturing partners with proven technical capability and a commitment to quality.
Frequently Asked Questions(FAQs)
What is a Non Ferrous Heat Exchanger Manufacturer?
A Non Ferrous Heat Exchanger Manufacturer designs and manufactures heat exchangers using corrosion resistant materials such as copper nickel, titanium, aluminium bronze and other specialised alloys for demanding industrial applications.
Why are non ferrous materials preferred in critical industries?
These materials provide excellent corrosion resistance, improved thermal conductivity and longer service life, making them suitable for harsh operating environments.
Which industries benefit most from non ferrous heat exchangers?
Oil & Gas, Petrochemicals, Fertilizers, Chemical Processing, LNG, FSRU, FPSO, Renewable Energy and Data Centre Cooling all benefit from reliable non ferrous heat exchanger solutions.
What certifications should a heat exchanger manufacturer have?
Manufacturers should ideally demonstrate compliance with recognised standards such as ASME, ISO quality management systems and relevant inspection and testing procedures.
How can buyers evaluate a reliable manufacturer?
Assess industry experience, engineering capability, manufacturing infrastructure, material expertise, quality certifications, testing procedures and after sales technical support before making a decision.













Sign in to leave a comment.